 Recycling and pelletizing
9 types
 Extrusion
8 types
 Mixing equipment
2 types
 Conveying and storage
8 types
 Drying and cooling
2 types
 Cutting, pressing and packaging
4 types
 Plastic processing machinery
3 types
 Electromechanical equipment
7 types
 Miscellaneous machinery
11 types
CONVEYOR BELTS
CONVEYOR BELTS
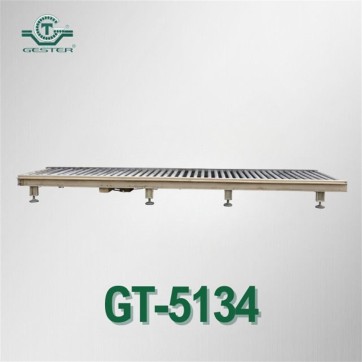
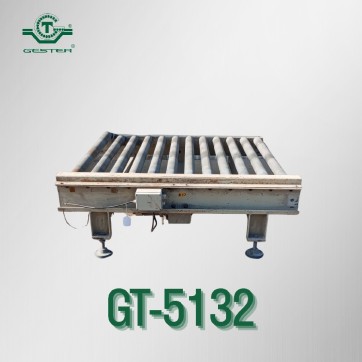
Powered roller conveyor belt 4,55
Power:
1.5 CV (1.1 KW)
+ info:
4,55 x 1,20 m
Type:
In stock
CONVEYOR BELTS
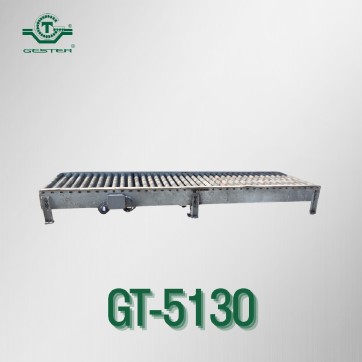
Powered roller conveyor belt 1,5 meter
Power:
1 CV (0.75 kW)
+ info:
1,5 x 1,20 m
Type:
In stock
CONVEYOR BELTS
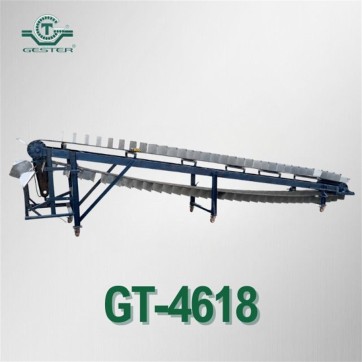
Powered roller conveyor belt
Power:
1.5 CV (1.1 KW)
+ info:
4,5 x 1,20 m
Type:
In stock
CONVEYOR BELTS
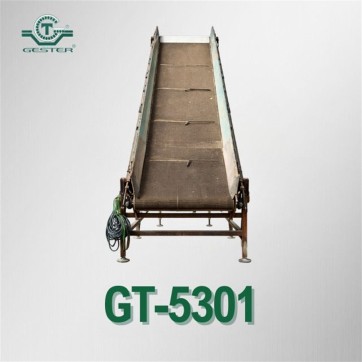
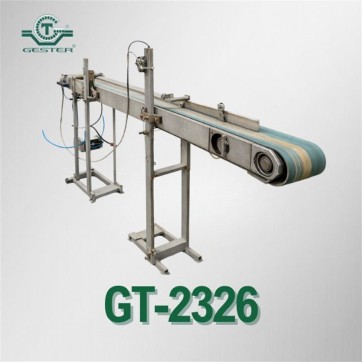
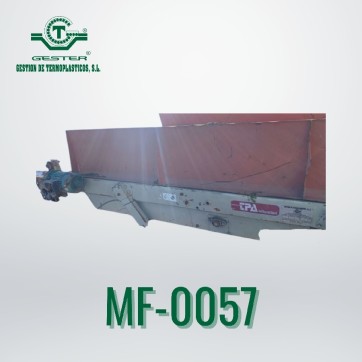
Conveyor belt 3.10 meter
Power:
Motor reductor: 2 CV (1.5 KW)
+ info:
3.10 x 1.40 m
Type:
En estado
Used Conveyor Belts
At Gester, we specialise in offering industrial conveyor belts that provide efficient and cost-effective solutions for a wide variety of sectors. Conveyor systems are a fundamental part of many logistics, manufacturing and processing operations, enabling materials and products to move continuously between different stages of a production line. Our catalogue includes high-quality used conveyor belts suitable for handling light products, bulk materials and heavier industrial loads.
Our used conveyor belts are carefully selected according to their condition, technical characteristics and potential application. Each available machine can be inspected and assessed to ensure that it provides reliable performance, allowing companies to access professional conveying equipment at a considerably lower cost than purchasing a new system.
Wide Range of Industrial Conveyor Belts
Conveyor belts form part of broader conveying and storage machinery installations used to automate material movement throughout industrial plants. By maintaining a consistent product flow, these systems can increase productivity, reduce manual handling and limit interruptions between processing stages.
At Gester, we understand that every production line has different requirements. The most suitable conveyor will depend on factors such as the material being transported, load weight, conveying distance, inclination, required speed and available installation space. Whether you need to move packaged products, plastic flakes, granules or industrial components, our equipment can provide a dependable material-handling solution.
Conveyor belts for specific processes: We offer equipment suitable for sectors such as plastics, recycling, food processing, logistics, warehousing and component manufacturing. In recycling facilities, conveyor belts are often installed before or after industrial shredders to feed plastic waste into the cutting chamber or transport the processed material towards subsequent stages.
Used conveyor belts: Choosing a second-hand conveyor can reduce investment costs while providing the performance required to expand, replace or improve an existing production line. Available systems may include horizontal conveyors, inclined conveyors, mobile belts and customised configurations for particular industrial applications.
Conveyor belts for flexible operations: Our catalogue includes different lengths, widths and structures that can be adapted to changing production needs. For materials that are better transported within an enclosed screw system, companies can also consider industrial augers as an alternative or complementary conveying method.
Conveyor Belts for Loading, Storage and Material Handling
Industrial conveyor belts can connect several areas of a facility, from material reception and storage to processing, inspection and dispatch. When raw materials are stored before entering the line, conveyors can be positioned beneath tanks and hoppers to receive a controlled discharge and move the material towards the next machine.
They are also useful for loading and unloading products from containers, workstations, platforms or packaging areas. Depending on the layout of the facility, conveyors may be combined with other transport and loading equipment to create a more complete internal logistics system.
A well-designed conveying installation can reduce bottlenecks and prevent unnecessary accumulation of material between processes. It can also help maintain a constant feed rate, which is particularly important when conveyor belts supply shredders, granulators, washing lines or other continuously operating machinery.
Benefits of Buying Used Conveyor Belts
Buying used conveyor belts from Gester is not only an economical choice, but also a strategic way to improve the efficiency of an industrial operation. Second-hand equipment can provide a faster solution for expanding production capacity, replacing an existing conveyor or automating a previously manual process.
Used conveyor belts may also offer shorter delivery times than newly manufactured systems, especially when the required equipment is already available in stock. This can help companies reduce downtime and implement improvements without waiting for a lengthy manufacturing process.
Choosing pre-owned machinery also contributes to the circular economy by extending the working life of industrial equipment. Instead of manufacturing a completely new system, a suitable used conveyor can be integrated into another facility and continue to provide productive service for years.
Our team can help you review important specifications such as belt width, total length, motor power, conveying speed, load capacity, inclination and construction materials. Assessing these factors makes it easier to select a conveyor belt that matches both the transported product and the configuration of the production line.
Frequently Asked Questions
Explore our available used conveyor belts and find a practical solution for improving material flow, reducing manual handling and connecting the different stages of your industrial process. Contact Gester for current availability, technical specifications or guidance on selecting the most suitable conveyor for your facility.
Last blog articles
Industrial Machinery Transport in Spain: Safe and Efficient Solutions
What Is an Extruder, How Does It Work, and What Is It Used For ?
HDPE or High-Density Polyethylene: What Is It, Properties, and Uses
Screw Compressor: What Is It, How It Works, Types, and Advantages
Indirect extrusion: what it is, how it works, and applications
See all